grandmark logoGrandmark International
@alexaseleno
Skip to main content

How to Choose Hex Machine Screws for Global Sourcing?

Global sourcing makes the Hex Machine Screw a specification challenge, not merely a price comparison. Grand View Research valued the global industrial fasteners market at approximately USD 90.04 billion in 2023. Its forecast reflects continued demand from automotive, machinery, electronics, and construction sectors. However, these figures cover broad fastener categories, not every Hex Machine Screw application. That distinction matters.

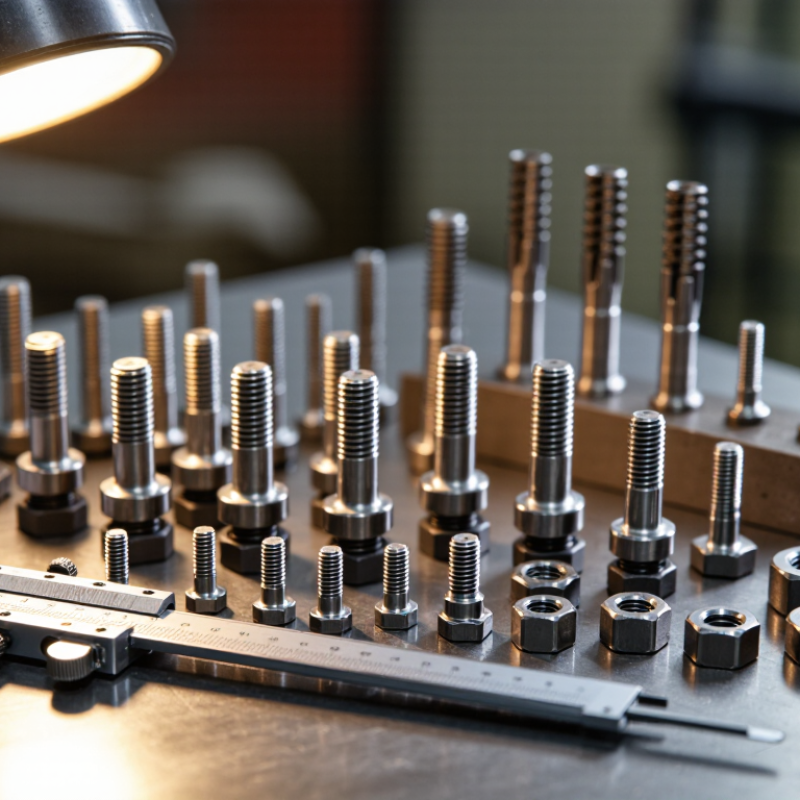
UN Comtrade trade data under HS 7318 can reveal shipment patterns, supplier concentration, and country-level trade values. Yet HS codes rarely identify thread class, drive geometry, plating, or tolerance. A reliable sourcing decision therefore requires more than a marketplace search. Buyers should compare ISO 898-1 mechanical requirements, ASME B18.6.3 dimensions, material certificates, salt-spray results, and lot traceability. Check the actual samples. Small details matter, including thread engagement, head height, burrs, and coating thickness.

John H. Bickford, author of An Introduction to the Design and Behavior of Bolted Joints, emphasized, “A bolted joint is only as good as its weakest component.” That principle applies directly to global procurement. A low-cost screw can fail through incorrect hardness, poor plating adhesion, or inconsistent gauges. The invoice may look attractive. The production line may disagree.

Experience also suggests that supplier audits and pre-shipment inspections reduce avoidable surprises. Still, no report replaces a tested sample in the buyer’s assembly. I would not treat any forecast as certainty. Markets shift, specifications are misread, and even experienced teams overlook one critical dimension. A careful sourcing plan connects data, standards, supplier evidence, and real-world fit before approving the Hex Machine Screw.

How to Choose Hex Machine Screws for Global Sourcing?

Define Thread, Head, and Drive Requirements Using ISO 68-1 and ISO 4762

How to Choose Hex Machine Screws for Global Sourcing?

A reliable specification starts with the thread. ISO 68-1 defines the basic profile for metric screw threads, including the flank angle and crest form. Write the complete designation, such as M8 × 1.25, rather than only stating “M8.” The pitch matters. A supplier may otherwise quote a coarse thread when your assembly requires a fine one. Thread tolerance should also be specified separately, often through the relevant ISO tolerance system.

The head and drive need equal attention. ISO 4762 covers hexagon socket head cap screws, including head dimensions and internal hexagon requirements. State the nominal diameter, screw length, head style, and socket size. Check whether the selected wrench or bit can reach the socket inside a narrow counterbore. A small clearance error can delay assembly.

Global sourcing adds practical risks. Different suppliers may interpret “socket screw” differently. Send a controlled drawing, thread callout, material requirement, and inspection points. Ask for sample parts before approving volume production. Measure thread pitch, head height, and socket depth with calibrated tools. I have seen specifications that looked complete but omitted thread tolerance. That omission created avoidable discussion. The checklist is not perfect. Review it against the actual assembly, not just the catalog description.

Select Metric or Unified Threads Under ISO 261, ASME B1.1, and Tolerance Classes

Choosing hex machine screws for global sourcing starts with the thread system, not the head shape.

ISO 261 covers preferred metric thread diameters and pitches. ASME B1.1 defines Unified inch threads, including UNC and UNF forms. Mixing them is not acceptable. A metric M6 screw cannot replace a 1/4-20 screw, even when both appear visually similar.

Tolerance classes control fit and production consistency. For metric screws, 6g external threads commonly mate with 6H internal threads under the ISO tolerance system. Unified threads often use 2A external and 2B internal classes. Tighter classes can improve alignment, but they may increase machining cost. In sourcing audits, coating thickness is often overlooked. It can reduce clearance and create assembly failures. Fit is not universal. A practical check should include thread gauges, pitch measurement, and a trial assembly with the actual nut or tapped hole.

Mordor Intelligence’s 2024 Fasteners Market analysis estimates the global fasteners market at about USD 89 billion in 2024, with continued growth toward 2029. That scale increases the value of standardized drawings and inspection records. However, market estimates differ between reports, so avoid treating forecasts as exact purchasing data.

Tips: State the standard, diameter, pitch, thread class, material, coating, and inspection method on every purchase order. Measure the mating part. Do not rely on appearance alone. When uncertain, request a first-article sample before approving bulk production.

Match Materials and Strength to ISO 898-1 Property Classes 8.8 and 10.9

When choosing hex machine screws for global sourcing, match the property class to the joint’s real load. ISO 898-1 class 8.8 screws typically provide 800 MPa nominal tensile strength and 640 MPa minimum yield strength. Class 10.9 raises these values to about 1,000 MPa and 900 MPa. That difference matters in compact assemblies, heavy clamping, and vibration-prone equipment.

Do not select class 10.9 only because it sounds stronger. Higher strength can reduce ductility and increase sensitivity to incorrect tightening or hydrogen embrittlement after certain surface treatments. Most 8.8 and 10.9 fasteners use quenched and tempered carbon or alloy steel, but the property class confirms performance, not a single chemical composition. Request material certificates, batch traceability, dimensional inspection, and independent tensile or hardness results. Check the head marking too. A missing or unclear marking deserves attention.

Tips: Confirm thread size, pitch, length, and tolerance before ordering. Compare the screw class with the matching nut and washer. Ask suppliers how plating is controlled. A certificate is useful, but it is not proof by itself. I have seen specifications copied incorrectly between drawings and purchase orders. Recheck every value against the latest standard and the actual application. Corrosion exposure also changes the decision, especially outdoors or near moisture. Sometimes a lower class with better corrosion control is safer than a stronger screw with poor installation discipline.

Specify Corrosion Protection with ISO 4042 Coating Thickness Requirements

How to Choose Hex Machine Screws for Global Sourcing?

Corrosion protection should be specified before requesting quotations. The NACE IMPACT Study estimated global corrosion costs at about US$2.5 trillion annually, equal to 3.4% of global GDP. That figure makes coating selection a commercial decision, not a cosmetic detail. In sourcing projects, I check the base material, thread size, washer contact, storage conditions, and installation environment. Coastal air demands more attention than a dry indoor warehouse.

ISO 4042:2018 provides a framework for electroplated coating systems on fasteners. It addresses coating designation, thickness, passivation, sealing, and hydrogen embrittlement relief. Avoid writing “zinc plated” alone. Specify the ISO 4042 coating system and its required minimum local thickness. The correct value depends on corrosion severity, fastener geometry, and thread tolerance. Excessive thickness can interfere with assembly. Too little protection can fail during transport.

Salt-spray hours need careful interpretation. ISO 9227 defines test methods, but laboratory hours do not directly predict outdoor service life. Ask suppliers for measured coating thickness, test records, and batch traceability. A magnetic thickness gauge can support incoming checks, although threaded surfaces remain difficult to measure consistently. I have seen specifications copy old thickness values without reviewing the application. That shortcut is convenient, but not reliable. Include inspection limits, sampling frequency, and rework rules in the purchase document.

How to Choose Hex Machine Screws for Global Sourcing?

Specify Corrosion Protection with ISO 4042 Coating Thickness Requirements

ISO 4042 zinc electroplated coating designations indicate the minimum local coating thickness in micrometres. For global sourcing, Fe/Zn5, Fe/Zn8, Fe/Zn12 and Fe/Zn25 represent increasing corrosion-protection thickness levels. Select the class according to the service environment, required durability and applicable corrosion-resistance testing; confirm the coating system and post-treatment with the supplier before approval.

Qualify Global Suppliers Through ISO 9001, PPAP, and ASTM F606 Testing

When sourcing hex machine screws globally, supplier approval should begin with evidence, not catalog photos. ISO 9001 certification indicates a controlled quality system, but it does not prove every screw meets your drawing. Ask for the certificate scope, recent audit status, process maps, calibration records, and nonconformance data. Check whether the certified site actually manufactures your parts. A certificate alone is not enough.

PPAP turns supplier claims into documented production evidence. Request the drawing, material certificates, dimensional results, process flow, control plan, FMEA, and capability studies where appropriate. For a hex screw, inspect thread class, head dimensions, drive fit, coating thickness, and lot traceability. Review samples from the intended production line. Not from a laboratory batch. That distinction matters. PPAP levels should match risk, volume, and application, rather than becoming paperwork for its own sake.

ASTM F606/F606M testing can verify mechanical performance for externally threaded fasteners. Depending on the specification, testing may include proof load, tensile strength, hardness, and wedge tensile strength. Confirm the test method, specimen condition, equipment calibration, and laboratory competence. Ask for lot-specific reports with clear acceptance criteria. Polished reports can hide unclear sampling plans. That weakness is easy to miss. Recheck it. Compare test results with your engineering requirements, not only the supplier’s standard. Remote audits, first-article inspection, and controlled change notification add practical protection. Still, no qualification process is perfect; field feedback may expose risks that documents never showed.

How to Choose Hex Machine Screws for Global Sourcing? - Qualify Global Suppliers Through ISO 9001, PPAP, and ASTM F606 Testing
Evaluation Dimension Applicable Standard or Reference Practical Requirement Supplier Evidence to Request Acceptance Criteria Priority
Product Geometry ISO 7045, ISO 7046, ISO 7047, or the specified national dimensional standard Confirm hex head diameter, head height, thread diameter, thread pitch, overall length, and drive dimensions against the approved drawing. Controlled product drawing, dimensional inspection report, gauge calibration records, and first-article samples. All critical dimensions conform to the drawing and the declared dimensional tolerance class. Mandatory
Thread Form ISO 965 series for metric threads; ASME B1.1 for unified inch threads Specify the thread system, nominal diameter, pitch or threads per inch, tolerance class, and whether the screw is fully or partially threaded. Thread plug-gauge records, thread inspection report, and sample verification using calibrated gauges. Thread gauges pass without excessive resistance, cross-threading, or incomplete engagement. Mandatory
Material and Grade ISO 898-1 for carbon and alloy steel fasteners; ISO 3506-1 for corrosion-resistant stainless-steel fasteners Choose the material and strength class according to the joint load, temperature, corrosion exposure, and galvanic compatibility. Material certificate, heat or lot traceability, chemical composition report, and mechanical-property report. Material designation, chemical composition, and mechanical properties match the purchase specification. Mandatory
Typical Strength Selection ISO 898-1 and ISO 3506-1 property-class requirements For example, property class 8.8 carbon-steel fasteners have a nominal minimum tensile strength of 800 MPa and a nominal minimum yield ratio of 0.8. A2-70 stainless fasteners have a minimum tensile strength of 700 MPa under ISO 3506-1. Lot-specific tensile, proof-load or yield, and hardness test results linked to the heat or production lot. Reported values meet the selected standard and the approved engineering specification; do not substitute classes without approval. Conditional
Mechanical Testing ASTM F606/F606M Use the applicable ASTM test procedures for externally threaded fasteners, including tensile strength, proof load or yield testing, hardness, and dimensional verification where applicable. Independent or qualified laboratory report identifying the sample, lot, test method, equipment, and actual results. Every required result meets the purchase specification and applicable material or property-class standard. Mandatory
Hardness Control ASTM F606/F606M and the selected ISO or national fastener standard Verify hardness using the scale and locations required by the applicable standard. Hardness must be consistent with the specified material and strength class. Hardness map or lot test report, test equipment calibration certificate, and sample identification. Measured hardness is within the permitted range and does not indicate over-hardening or an incorrect grade. Mandatory
Quality Management System ISO 9001:2015 Prioritize suppliers operating a documented quality management system covering contract review, purchasing, production control, inspection, nonconformity, corrective action, and record retention. Current ISO 9001 certificate, certification scope, validity dates, issuing certification body, and audit status. Certificate is current, the scope covers fastener manufacturing or relevant processing, and the legal manufacturing site is identified. Recommended
Process Approval Customer-specific quality requirements and documented process controls Review forming, machining, heat treatment, thread rolling or cutting, coating, sorting, and final packing controls before approving the supplier. Process flow chart, PFMEA, control plan, work instructions, inspection plan, and process-capability results for critical characteristics. Critical operations have defined controls, reaction plans, and traceable inspection records. Mandatory
PPAP Submission AIAG PPAP framework or an equivalent customer-approved submission process Require a PPAP package when the screw is safety-critical, newly sourced, changed in design or process, or produced at a new manufacturing location. Part submission warrant, approved drawing, material records, dimensional results, test results, process documents, and sample parts as applicable. Submission level is agreed before production; all deviations are documented and formally approved. Recommended
PPAP Submission Levels AIAG PPAP level structure Use the customer-defined level: Level 1 generally requires a warrant and limited supporting data, while Levels 2 through 5 require progressively more supporting records and may include on-site review. Written customer requirement, completed submission checklist, and evidence corresponding to the agreed level. The supplier submits the complete package at the agreed level before mass production or shipment approval. Conditional
Coating and Corrosion ISO 4042 for electroplated coatings; ASTM B117 for neutral salt-spray testing when specified Define coating type, coating thickness, corrosion requirement, hydrogen-embrittlement controls, and prohibited substances before quotation. Coating certificate, thickness measurements, salt-spray report where required, plating-process records, and embrittlement-relief evidence for high-strength parts. Coating, thickness, appearance, corrosion performance, and embrittlement controls meet the approved specification. Conditional
Torque and Clamp Load Customer engineering specification; applicable torque-tension test method Do not select installation torque from a generic chart alone. Confirm the relationship between torque, friction, preload, coating, lubrication, and joint design. Torque-tension test data, lubricant or coating details, installation instructions, and agreed preload range. Measured clamp load reaches the design target without thread stripping, head failure, or unacceptable scatter. Conditional
Traceability ISO 9001:2015 documented-information controls and customer requirements Maintain traceability from raw material heat through forming, heat treatment, coating, inspection, packing, and shipment. Lot number, heat number, production date, machine or line identification, inspection records, and packing labels. Each shipment can be traced to a defined production lot and its supporting quality records. Mandatory
Sampling and Inspection Customer sampling plan; ISO 2859-1 may be used for attribute sampling when agreed Define inspection frequency for dimensions, thread fit, appearance, hardness, coating, and mechanical properties. Critical characteristics may require 100% sorting. Approved inspection plan, sampling rationale, inspection results, nonconformance records, and sorting reports. Sampling is agreed in writing, measurement systems are suitable, and critical defects are controlled to zero acceptance where specified. Mandatory
Packaging and Logistics Customer packaging specification and agreed Incoterms Protect threads and plated surfaces from impact, moisture, contamination, mixing, and label loss during international transport. Packaging specification, pallet or carton test evidence where required, packing photographs, and shipping-label format. Correct part number, lot number, quantity, country-of-origin information, and protection are maintained through delivery. Recommended
Change Control ISO 9001:2015 operational control and customer-specific requirements Require advance notification and approval for changes to material, dimensions, tooling, heat treatment, coating, subcontractors, production site, or inspection method. Change-notification procedure, revision history, requalification plan, and updated PPAP or test results when applicable. No controlled change is implemented without documented risk review and customer approval where required. Mandatory
Supplier Scorecard Purchaser-defined supplier performance metrics Monitor quality, delivery, responsiveness, corrective-action effectiveness, documentation accuracy, and cost stability after qualification. Monthly or quarterly performance data, corrective-action closure records, and trend charts by product and lot. Supplier maintains agreed targets and demonstrates timely, evidence-based corrective action for recurring issues. Recommended
Note: The applicable product, material, coating, testing, sampling, and PPAP requirements should be stated in the purchase specification and approved drawing. Where standards conflict, the customer-approved engineering specification and the legally applicable requirement should govern.